Producing high-purity water can become costly when a plant depends on repeated acid and caustic regeneration, frequent shutdowns, or unstable ion exchange performance. Electrodeionization solves much of this problem by combining resin, selective membranes, and electricity into one continuous purification process.
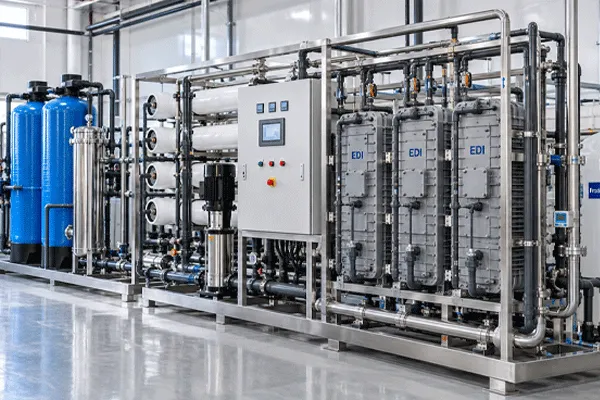
Electrodeionization, or EDI, is a continuous water treatment technology that removes dissolved ions from highly pretreated water. It combines ion exchange resin, ion exchange membranes, and a direct-current electric field. EDI is normally installed after reverse osmosis to polish RO permeate into high-purity or ultrapure water without routine chemical regeneration of the resin.
Electrodeionization (EDI) in Water Treatment: How It Produces High-Purity Water
Article Outline
- What is electrodeionization in water treatment?
- What is the working principle of EDI?
- What happens inside an EDI module?
- Why is reverse osmosis normally installed before EDI?
- How does EDI compare with traditional ion exchange?
- What are the benefits of using electrodeionization?
- What water quality can an EDI system produce?
- What feed water does an EDI system need?
- Where is electrodeionization technology used?
- How should an electrodeionization system be designed?
- How is EDI operated and maintained?
- Frequently asked questions
What Is Electrodeionization in Water Treatment?
Electrodeionization, usually shortened to EDI, is a high-purity water treatment process designed to remove dissolved ionic substances from water.
The process combines three technologies:
- Ion exchange resin
- Ion exchange membranes
- A direct-current electrical field
Unlike a conventional deionization unit, the resin inside an EDI module does not normally need to be taken offline for routine acid and caustic regeneration. Electricity helps move unwanted ions away from the product-water stream while continuously supporting resin regeneration.
DuPont describes EDI as a continuous process for polishing reverse osmosis permeate using DC current. Veolia likewise describes continuous electrodeionization as a self-regenerating process that combines resin, membranes, and electricity.
A simplified industrial process looks like this:
Raw Water
    ↓
Pretreatment
    ↓
Reverse Osmosis
    ↓
RO Permeate
    ↓
EDI
    ↓
High-Purity Water
For many industrial water systems, EDI therefore acts as the final demineralization or polishing stage rather than the first treatment step.
What Is the Working Principle of EDI?
The working principle of EDI sounds complex, but the basic idea is easy to understand.
RO permeate flows through chambers filled with ion exchange resin. These chambers sit between special cation- and anion-selective membranes. When the EDI system applies an electrical potential, dissolved ions start moving according to their charge.
Positive ions, or cations, include:
- Sodium
- Calcium
- Magnesium
- Ammonium
Negative ions, or anions, can include:
- Chloride
- Sulfate
- Nitrate
- Bicarbonate
- Ionized silica species under suitable conditions
The electric field drives these ions from the water toward the appropriate ion exchange membranes.
Simplified EDI Process
                   DC Electric Field

        Anode (+)                    Cathode (-)
             ← Anions        Cations →

   ┌───────────────────────────────────────┐
   │       Resin-Filled Dilute Chamber     │
   │                                       │
   │       RO Permeate Enters              │
   │               ↓                       │
   │       Dissolved Ions Removed          │
   │               ↓                       │
   │        Purified Water Leaves          │
   └───────────────────────────────────────┘
          ↓                         ↓
    Concentrate Stream        Product Water
The ion exchange resin provides a conductive path that helps the ions migrate toward the membranes.
This is an important difference between ordinary electrodialysis and EDI. As water becomes very pure, it conducts electricity less easily. Adding resin helps maintain effective ionic transport even when the water has very low conductivity.
What Happens Inside an EDI Module?
An EDI module contains several components working together.
| EDI Component |
Main Function |
| Ion exchange resin |
Captures ions and provides conductive pathways |
| Cation exchange membrane |
Allows selected positive ions to migrate |
| Anion exchange membrane |
Allows selected negative ions to migrate |
| Dilute chamber |
Carries water being purified |
| Concentrate chamber |
Receives removed ionic contaminants |
| Electrodes |
Create the DC electric field |
| Flow distributors |
Maintain controlled hydraulic flow |
| Module housing |
Protects the internal EDI stack |
The dilute chambers contain the water that will become product water. The concentrate channels carry removed ionic species away from the purified stream.
The resin performs two important jobs.
First, it exchanges ions with the water, similar to traditional ion exchange.
Second, it creates conductive pathways that help ions move through the EDI stack under the applied electric field.
How Does the Resin Regenerate Continuously?
This is one of the most important features of EDI technology.
Under suitable electrical conditions, a small amount of water splits into hydrogen ions, H⁺, and hydroxide ions, OH⁻.
These ions help regenerate the ion exchange resin during operation.
The result is continuous electrodeionization.
A traditional regenerable mixed bed eventually becomes exhausted and must be restored using acid and caustic chemicals. EDI instead uses electricity to maintain the deionization process while the system is running.
This does not mean the complete plant will never need chemicals. RO pretreatment, cleaning, pH control, sanitization, or scale prevention may still require chemical treatment.
Why Is Reverse Osmosis Normally Installed Before EDI?
EDI works best with already purified feed water.
This is why reverse osmosis is normally installed upstream.
RO removes most dissolved salts and reduces the ionic load before water reaches the EDI process. The EDI unit then removes the smaller residual ion load that remains in the RO permeate.
Think of the two systems as doing different levels of work:
RO = bulk desalination
EDI = final ionic polishing
DuPont specifically describes EDI as a technology for deionizing RO permeate, while Veolia’s RO/CEDI systems combine the two processes to produce high-purity deionized water continuously.
Typical Industrial Treatment Train
Raw Water
   ↓
Sand / Multimedia Filtration
   ↓
Activated Carbon or Other Pretreatment
   ↓
Security Filtration
   ↓
UF, If Required
   ↓
Reverse Osmosis
   ↓
Optional Second-Pass RO / CO₂ Control
   ↓
EDI
   ↓
UV / Final Polishing, If Required
   ↓
High-Purity Water Tank
For demanding projects, engineers may use double-pass RO, membrane degassing, or pH adjustment before EDI.
This is especially important because substances such as carbon dioxide, residual hardness, silica, and ionic loading can affect EDI performance. DuPont’s EDI technical guidance specifically identifies feed-water quality, power, flow, and pressure balance as important design factors.
How Does EDI Compare With Traditional Ion Exchange and Mixed Bed Systems?
Traditional deionization commonly uses cation and anion exchange resin.
A mixed-bed system combines both resin types to achieve very low conductivity.
The problem is regeneration.
Once conventional resin becomes exhausted, it must be restored using chemical regenerants. This may require acid, caustic, chemical storage, operator handling, neutralization, wastewater disposal, and downtime.
EDI changes that operating model.
| Feature |
EDI |
Traditional Mixed Bed |
| Ion exchange resin |
Yes |
Yes |
| Ion exchange membranes |
Yes |
No |
| DC electricity |
Yes |
No |
| Routine chemical regeneration |
Normally no |
Yes for regenerable systems |
| Continuous operation |
Yes |
Interrupted by regeneration unless redundant beds are used |
| Best feed |
RO permeate |
Can handle broader conditions depending on design |
| Automation potential |
High |
Moderate to high |
| Chemical handling |
Reduced |
Higher |
| Product quality |
High / ultra-high under suitable conditions |
High / ultra-high |
DuPont identifies EDI as an alternative to conventional mixed-bed ion exchange for polishing RO permeate. The main operational advantage is the elimination of routine acid and caustic regeneration.
However, traditional ion exchange still has useful applications.
A mixed bed may be preferred when feed conditions, intermittent operation, extreme polishing requirements, plant design, capital cost, or existing infrastructure make it more suitable.
Good engineering does not mean choosing EDI for every project.
It means selecting the correct treatment technologies for the required water specifications.
Electrodeionization (EDI) in Water Treatment: How It Produces High-Purity Water
What Are the Benefits of Using Electrodeionization?
The main benefits of using electrodeionization come from continuous operation and reduced regeneration requirements.
1. Continuous High-Purity Water Production
EDI can operate continuously while the resin regenerates electrically.
That makes it useful for factories where stopping water production interrupts manufacturing.
2. Reduced Chemical Regeneration
Traditional regenerable resin beds require acid and caustic chemicals.
EDI normally avoids this routine regeneration step.
This can reduce:
- Chemical storage
- Chemical handling
- Operator exposure
- Regeneration wastewater
- Regeneration downtime
3. Stable Product Quality
A correctly designed EDI system can provide stable water quality without the quality cycle associated with resin exhaustion and regeneration.
4. Easy Automation
EDI fits well into automated water treatment systems.
Instrumentation may monitor:
- Product conductivity
- Resistivity
- Voltage
- Current
- Flow rate
- Feed pressure
- Concentrate pressure
- Temperature
These signals can be integrated into PLC or SCADA systems.
5. Compact Integration
EDI modules are relatively compact compared with some traditional demineralization arrangements.
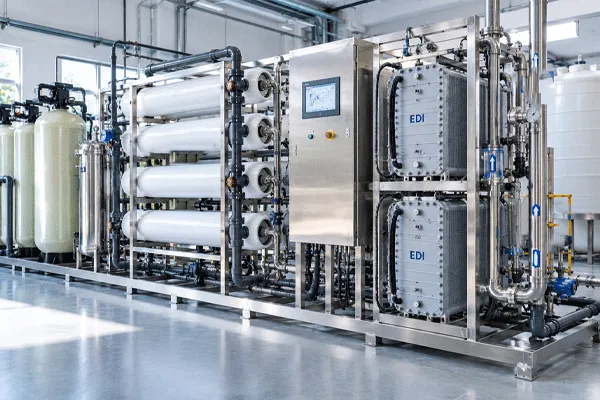
This makes them useful in skid-mounted and containerized water purification system designs.
For EPC contractors, factory assembly can also reduce field piping, electrical work, and commissioning complexity.
What Water Quality Can an EDI System Produce?
EDI is widely used for high purity water production.
Commercial systems can produce very low-conductivity water when they receive suitable RO permeate and operate within their specified conditions.
DuPont states that its EDI technology can produce product water up to approximately 18 MΩ·cm under suitable operating conditions. Veolia also offers integrated RO/CEDI equipment designed to produce highly deionized water at similar purity levels.
This is close to the upper resistivity range associated with extremely pure water.
However, the number should not be treated as an automatic guarantee for every installation.
Actual purity depends on:
- RO permeate quality
- Feed conductivity
- CO₂
- Silica
- Hardness
- Temperature
- Flow rate
- Electrical loading
- Module design
- System recovery
For this reason, EPC specifications should define a required product-water quality and then select the module and pretreatment around that requirement.
Conductivity vs. Resistivity
High-purity water is commonly measured using resistivity rather than only conductivity.
Higher resistivity generally indicates fewer ionic impurities.
For example:
More Dissolved Ions
        ↓
Higher Conductivity
        ↓
Lower Resistivity

Fewer Dissolved Ions
        ↓
Lower Conductivity
        ↓
Higher Resistivity
An EDI supplier should clearly state the design basis used for high purity water production, not simply advertise a maximum laboratory value.
What Feed Water Does an Electrodeionization System Need?
Feed-water control is one of the most important parts of EDI design.
An electrodeionization system cannot simply accept untreated tap water, surface water, or brackish water.
The EDI unit normally receives RO permeate.
Important parameters can include:
- Conductivity
- Hardness
- CO₂
- Silica
- TOC
- Chlorine or other oxidants
- Temperature
- Feed pressure
- Ionic load
DuPont’s technical manual highlights total exchangeable anions, CO₂, hardness, silica, flow, power, and pressure differential as important design considerations.
Why does this matter?
Because poor feed quality can lead to:
- Scaling
- Higher electrical resistance
- Lower product resistivity
- Unstable current
- Increased pressure drop
- Membrane damage
- Resin fouling
- Reduced module life
CO₂ Is Easy to Overlook
Carbon dioxide is a common design issue.
RO may remove most ionic salts very effectively, but dissolved CO₂ behaves differently. Excessive CO₂ can increase the ionic load handled by the EDI system.
Depending on the project, engineers may control it through:
- pH adjustment before RO
- Membrane degassing
- Additional RO treatment
- Other process optimization
This is why a proper design review should consider more than one conductivity number.
Electrodeionization (EDI) in Water Treatment: How It Produces High-Purity Water
Where Is Electrodeionization Technology Used?
Electrodeionization technology is mainly used where industries require continuous, reliable high-purity water.
Semiconductor and Electronics Manufacturing
Microelectronics production requires very low ionic contamination.
EDI may form part of an ultrapure water plant that also includes RO, UV, polishing, degassing, and final filtration.
Pharmaceutical and Biotechnology Plants
Pharmaceutical facilities use carefully designed purified-water systems.
EDI can form part of systems producing Purified Water and may also be integrated upstream within systems designed around water for injections requirements, subject to the applicable pharmacopoeia, process design, sanitization strategy, and regulatory requirements.
EDI alone should not be described as automatically producing compliant WFI.
Power Generation
Boiler makeup water requires very low mineral loading to help control scale, deposition, and corrosion.
DuPont lists EDI as a polishing technology for boiler-feed-water applications and describes it as capable of continuous high-purity production.
Chemical and Process Industries
Sensitive processes often need controlled process water so dissolved ions do not interfere with products or reactions.
Hydrogen and Advanced Manufacturing
High-purity feed water is also becoming important in electrolysis and advanced energy applications.
Veolia, for example, uses RO and EDI together in purification systems designed for hydrogen-production applications.
Other applications can include:
- Laboratories
- Cosmetics manufacturing
- Food and beverage processes
- Battery manufacturing
- Precision cleaning
- Industrial utility water
- High-purity chemical preparation
How Should an EDI Water Treatment System Be Designed?
A reliable EDI water system begins upstream.
The designer should not start by asking, “Which EDI module should I buy?”
Start with:
- Raw-water analysis
- Required product-water specification
- Required flow rate
- Operating schedule
- RO recovery and permeate quality
- CO₂ and hardness control
- Required redundancy
- Automation requirements
Then size the EDI stage.
Illustrative Engineering Example
Consider an industrial facility that needs continuous high-purity water for sensitive manufacturing.
The process might use:
Raw Water
   ↓
Pretreatment
   ↓
UF
   ↓
Two-Pass RO
   ↓
CO₂ Control
   ↓
EDI
   ↓
UV
   ↓
Final Filter
   ↓
High-Purity Water Storage & Distribution
The RO system performs the main water desalination work.
The EDI stage then removes residual ionic contaminants.
Final treatment protects water quality in storage and distribution.
This type of integrated design is more reliable than treating each technology as an isolated piece of equipment.
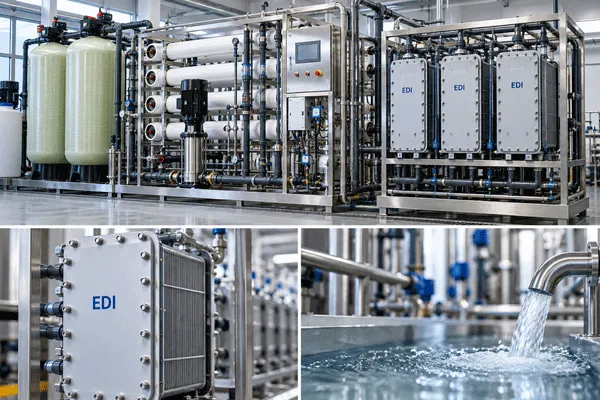
As a manufacturer and engineering-oriented water-treatment supplier, this is also how we approach EDI projects. We can integrate RO membranes, EDI modules, UF pretreatment, pumps, instruments, tanks, piping, PLC controls, and skid or container structures into a complete system.
For EPC contractors, that can simplify interface management during installation and commissioning.
How Is an EDI System Operated and Maintained?
EDI usually requires less routine regeneration work than a traditional ion-exchange plant.
But “low maintenance” does not mean “no maintenance.”
Operators should monitor:
- Product conductivity or resistivity
- Feed conductivity
- Module voltage
- Current
- Product flow
- Concentrate flow
- Feed pressure
- Pressure differential
- Temperature
Trends often tell more than one isolated reading.
For example, a gradual decline in product resistivity together with a rise in pressure drop may indicate a feed-water or fouling problem.
Can an EDI Module Be Cleaned?
Yes, depending on module design and supplier procedures.
Although EDI avoids routine chemical resin regeneration, a module can still suffer from scale, organic contamination, biological fouling, or silica-related problems if feed-water conditions fall outside specifications.
DuPont’s technical guidance includes cleaning considerations for EDI modules.
The better approach is prevention.
Stable RO operation, correct pretreatment, good instrumentation, and proper feed-water control usually provide better economics than repeatedly cleaning a poorly protected EDI stage.
EDI vs. Other Water Purification Techniques
Choosing among different water purification techniques depends on the contaminant and the final water quality required.
| Technology |
Primary Function |
Typical Position |
| UF |
Removes particles and microorganisms |
Pretreatment |
| RO |
Removes most dissolved salts |
Main desalination |
| EDI |
Removes residual ionic impurities |
RO polishing |
| Mixed bed |
Deep ionic polishing |
Final polishing |
| UV |
Microbial / TOC-related control depending on wavelength |
Post-treatment |
| Final membrane filter |
Particle and microbial control |
Distribution polishing |
The technologies are often complementary.
UF protects RO.
RO protects EDI.
EDI produces highly deionized water.
Post-treatment helps preserve quality.
This is why modern industrial water plants should be viewed as integrated water solutions, not a collection of unrelated filters.
Frequently Asked Questions About Electrodeionization
What does EDI mean in water treatment?
EDI means electrodeionization. It is a continuous deionization process that combines ion exchange resin, ion-selective membranes, and direct electrical current to remove ionic contaminants from highly pretreated water.
Can EDI replace reverse osmosis?
No. In most industrial applications, EDI is installed after reverse osmosis.
RO performs bulk dissolved-salt removal, while EDI polishes the remaining ionic impurities to produce high purity water.
Can EDI replace a mixed bed?
In many RO-permeate polishing applications, EDI can replace conventional regenerable mixed-bed ion exchange.
The benefit is continuous operation without routine acid-and-caustic resin regeneration. However, feed-water limits, investment cost, operation mode, and product requirements must still be evaluated.
Does EDI use chemicals?
The EDI process normally does not require the routine acid and caustic regeneration used in conventional regenerable ion exchange.
However, the overall plant may still use chemicals for RO pretreatment, pH correction, cleaning, scale control, or sanitization.
Can EDI produce ultrapure water?
Yes, EDI can form an important part of systems designed to produce ultrapure water. Commercial EDI technologies can approach approximately 18 MΩ·cm under suitable conditions.
Final achievable quality depends on feed water, system design, temperature, operating conditions, and downstream polishing requirements.
What is the difference between an EDI module and an EDI system?
An EDI module is the core separation device containing resin, membranes, and flow channels.
An EDI system or skid includes the module plus:
- DC power supply
- Piping
- Valves
- Instruments
- Controls
- Flow regulation
- Electrical components
- Structural frame
The complete system allows the module to operate safely and consistently within an industrial water plant.
Final Thoughts: Why EDI Matters for High-Purity Water Production
Electrodeionization has changed the way many industries approach final demineralization.
Instead of repeatedly exhausting and chemically regenerating resin beds, continuous EDI combines membrane separation, ion exchange, and electricity to remove residual ions while regenerating the resin during normal operation.
Its strongest application is after RO.
That pairing creates a logical division of work:
Reverse Osmosis → Bulk Salt Removal
EDI → Final Ionic Polishing
For semiconductor plants, pharmaceutical facilities, power stations, chemical plants, advanced manufacturing operations, and other projects with demanding water purification needs, the result can be a compact and highly automated route to continuous high-purity water production.
As a manufacturer of hollow fiber UF membranes, RO membranes, EDI modules, pure-water systems, ultrapure-water systems, and integrated water-treatment plants, we design the entire treatment train around feed-water quality and final water specifications—not around one piece of equipment.
For EPC contractors and industrial users, this means the EDI stage can be integrated with RO, pretreatment, tanks, pumps, instruments, PLC/SCADA controls, skid structures, and commissioning support as one engineered system.
Key Things to Remember
- EDI stands for electrodeionization.
- EDI combines ion exchange resin, ion exchange membranes, and DC electricity.
- It continuously removes dissolved ionic contaminants from pretreated water.
- Electrical conditions help regenerate the resin during operation.
- EDI therefore avoids routine acid-and-caustic regeneration of a conventional mixed bed.
- Reverse osmosis normally comes before EDI.
- RO performs bulk desalination; EDI performs final ionic polishing.
- Feed-water quality strongly affects EDI performance.
- Hardness, CO₂, silica, conductivity, temperature, and ionic load should be reviewed during design.
- EDI can produce very high-purity water under suitable operating conditions.
- EDI is widely used in semiconductor, pharmaceutical, power, chemical, laboratory, and advanced manufacturing applications.
- An EDI module is only one component; a complete EDI system also needs power, piping, controls, instruments, and hydraulic management.
- “Chemical-free regeneration” does not mean the entire water-treatment plant will never use chemicals.
- The most reliable high-purity plant is designed as an integrated RO + EDI water purification system.
Technical Sources
- DuPont – Electrodeionization (EDI): technical explanation of RO-permeate polishing, ion exchange resin, ion-selective membranes, electrical current, and continuous resin regeneration.
- DuPont EDI-310 Technical Manual: feed-water requirements and design considerations including ionic loading, CO₂, hardness, silica, flow, power, and pressure.
- Veolia Water Technologies – Continuous Electrodeionization: explanation of continuous EDI as a self-regenerating RO-permeate polishing process.
- DuPont – Boiler Feed Water Treatment: industrial use of EDI for continuous high-purity water polishing.

 11:13